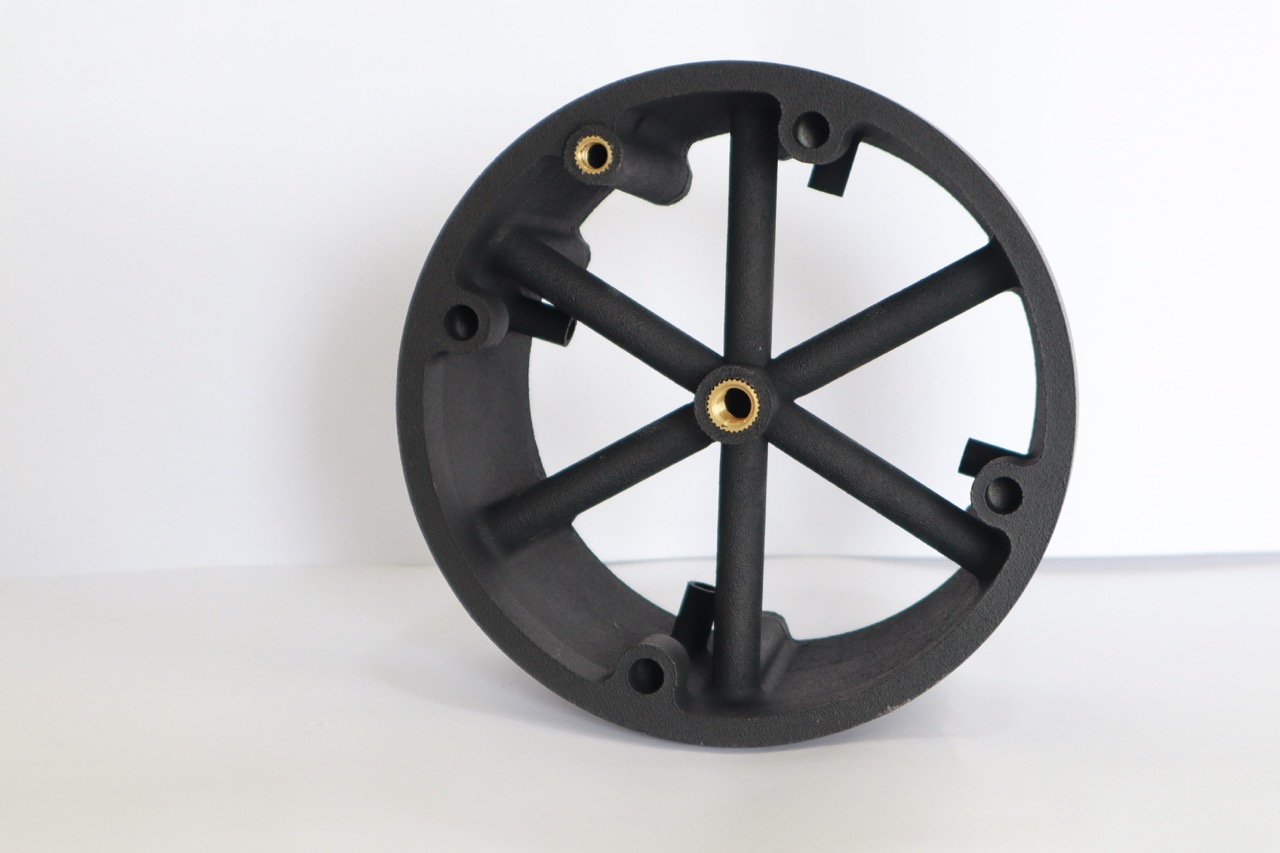
3D Print Snap Fit Joints: From First Sketch to Final Part
If you've ever popped a plastic lid into place without reaching for a screwdriver, you've used a joint like this. These small, flexible features click two parts together, skipping fasteners or adhesive altogether. As additive manufacturing has matured, they've moved past hobby projects into electronics housings, automotive brackets, medical casings, and industrial enclosures that get opened and closed hundreds of times over a product's life. The use of snap-fit features instead of screws shaves real assembly time off a production line, too.
Get the geometry wrong, though, and a joint like this cracks the third time someone uses it, not the three-hundredth. This guide covers the design principles, tolerances, materials, and printing technology that hold up in daily use, plus the most common reasons these connections fail and how to prevent it.
What Are Snap-Fit Joints?
A snap-fit joint is a mechanical connection built into the part itself instead of added afterward. One side carries a flexible arm, bead, or hook; the other a groove or lip. Push them together, the feature deflects, clears the lip, and springs back to lock the assembly shut. No screws, no adhesive, no separate hardware.
Every joint type works the same way: something bends, catches, and holds. A functional snap-fit for a battery door behaves nothing like one built into a sealed enclosure that never opens again, and getting that distinction right early in product design saves a lot of reprinting.
How to Design Snap-Fit Joints for 3D Printing
3D printing isn't injection moulding with a different machine attached. A mould's fixed cavity controls how plastic flows and cools; a printed structure has to flex thousands of times on its own. HP Multi Jet Fusion, or MJF, is the process we lean on most, since it fuses powder across the full build area rather than depositing material line by line, which changes how you should think about strength from the first 3D model onward.
Snap-Fit Design Principles
Good design here comes down to a handful of specs, not guesswork:
- Beam taper: taper the arm from base to tip so stress spreads evenly, not piling up at one point.
- Root fillet: add a fillet where the arm meets the base. It's the single biggest lever against cracking; a sharp inside corner is where nearly every broken joint starts.
- Minimum thickness of 1 mm at the cantilever base for parts like these. Thinner and the arm loses its grip; much thicker and it snaps instead of flexing.
- Hook depth: size the hook so material never bends past its elastic limit during engagement. Undersize it and the joint won't hold; oversize it and every insertion risks a crack.
- Deflection axis: let the cantilever arm flex in the X-Y plane where orientation allows, not along the layer lines running through the Z axis, where the load path is weakest.
These aren't arbitrary numbers. They come from HP's own design guidelines for this process, checked against how parts fail on our shop floor and against published guidance from sources like Protolabs Network.
Before locking the final design, run a quick design validation pass: print a low-cost test coupon of just the joint and cycle it by hand thirty or forty times, checking for whitening or cracking at the root. It's a five-minute check that catches most risk of failure early, and one of the best practices for designing parts like this that too many teams skip.
Reusable vs Permanent Joints
A reusable design needs a gentler approach since engineers assemble and disassemble it many times, not just once. A permanent one can afford a sharper hook, since the halves only need to snap together once. Either way, a tight snap-fit assembly right out of the box beats a loose one that needs extra glue.
Types of Snap-Fit Joints
Different geometries call for different types of 3D printed snap connections, and most engineers only need the three broad types of snap fit joints below. Once you understand these snap-fit types, picking the right design gets easier.
Cantilever
The cantilever snap-fit joint is the most common: a straight arm that bends outward when pushed into a slot. It's predictable, easy to model in CAD, and ideal for control panels and battery compartments. Cantilever snap-fits handle most enclosure designs we see, and snap-fit cantilevers dominate consumer electronics for the same reason: a straight arm is easiest to calculate and most forgiving to print.
Annular
An annular joint is the ring-shaped version. A circular bead on a cylindrical part is sized to protrude just enough to expand or contract into a matching groove, the way pen caps and bottle lids do, anywhere a round part needs this kind of connection instead of a straight edge.
Torsional
Torsional joints twist rather than bend straight. A flexible arm connects to a torsion bar that rotates under pressure from a lever, ideal for quick-release luggage clasps and flip-top closures that need deliberate motion to open. Some engineers group ball joints into this family too, though a true ball joint uses a spherical socket and behaves differently under repeated cycling.
Snap-Fit Tolerance for 3D Printing
Snap fit tolerance for 3D printing is where most first attempts go wrong, since rules for machined shafts and holes don't transfer directly to a printed part, and that's not true of every 3D printing process. For this process, the numbers that hold up are:
- Mating gap: at least 0.4 mm between interlocking surfaces, with roughly ±0.2 mm tolerance per part.
- General clearance: at least 0.7 mm between assembly faces that aren't directly interlocking.
- Dimensional accuracy: about ±0.2 mm up to 100 mm, and 0.2% of the dimension above that, measured after sandblasting.
These figures come from HP's official handbook for this printing technology, not a generic tolerance chart from a different process. Tolerancing this tightly matters more here than almost anywhere else, since a connection that's 0.1 mm too tight can be the difference between a smooth click and a hairline crack on day one.
Best Material for 3D Printed Snap Fits
Material choice decides whether a joint like this survives real use or cracks by the tenth cycle. Regular PLA and standard rigid plastics usually can't take it; they're too brittle and don't recover shape after repeated flexing.
Nylon-based materials do much better. PA12 offers strength and tighter accuracy for stiffer designs; PA11 is more ductile, holding onto flexibility and fatigue resistance through more open-close cycles. Amuse3D prints both grades for industrial snap-fit components, chosen by cycle count, and ships these 3D printed parts to customers across India, the US, the UK, and beyond, so a part that holds up in Chennai has to survive a long shipment too.
For FDM, a strain-resistant filament such as nylon or TPU beats a plain default material, since printed layers inherit weak spots that a flex point eventually finds. For resin printing, pick a tough, flexible SLA resin over a standard rigid one; most default options are accurate but too brittle for a connection that has to move.
3D Printing Technology for Snap-Fit Joints
The printing technology behind a joint like this matters as much as the material. FDM and SLA both build parts in flat layers, so the bond between layers is often weaker than the plastic itself, an effect called anisotropy: strength that changes depending on which direction you pull.
This process, described earlier, sidesteps that problem by fusing powder across the entire bed instead of depositing material line by line, so parts come out closer to isotropic. In industrial 3D printing, that's the whole reason this process exists as an alternative to FDM; the strength gap between anisotropic and isotropic 3D-printed parts becomes obvious the first time a joint fails in the field. It's why we route most functional assemblies, and increasingly full functional 3D printed assemblies, through this technology. Most 3D printed snap-fits we manufacture for repeat customers use one of these two nylon grades for exactly this reason.
Why Snap Fits Break (and How to Fix Them)
The most common snap-fit failure by far is a cracked root, not a broken hook. Sharp internal corners concentrate stress until a crack starts, printing in the wrong orientation weakens the layer bond right where the arm needs to flex, and pushing a connection past its intended deflection breaks it outright even in a well-made design.
The fix is rarely a new material. It's usually a fillet that's too small, a beam too short for the deflection it handles, or a hook depth that assumes more give than the geometry has. Longer beams, bigger fillets, a springier material, and a printing technology built for parts with snap-fit demands like this one solve most of these problems without a full redesign.
When to Move from Snap Fits to Injection Moulding
For early builds and small runs, 3D printing wins on cost and lead time since you can test a change overnight instead of waiting on tooling. Once volume climbs, injection molded parts become the more economical choice, and CNC machining services help validate the tooling before a full run completes.
Amuse3D supports that transition: we help carry a proven joint geometry from an early 3D printed prototype into an injection moulding tool without redesigning it, so the part that passed cycle testing is the part that ships. Whether you 3D print snap-fit test parts first or go straight to production, the same tolerances apply. We've found 3D printing snap-fit joints as physical test coupons catch problems no simulation does.
Instant quote for your next batch of custom parts, or send your design file and our design team will flag any geometry that needs a second look before it prints. Designing snap-fit joints for parts that ship worldwide means accounting for material shrinkage and packaging stress too, not just the print settings.
Conclusion
Proper design here comes down to a short list of fundamentals: a tapered beam, a real fillet at the root, the right material for the cycle count you need, and a printing technology that doesn't leave weak spots along the way it was built. Get those right and a connection like this holds up for years, not weeks.
If you're ready to move from concept to a working part, Upload parts and Amuse3D's team will review the geometry, confirm tolerances, and get a test print in your hands fast.
FAQs
Can 3D printed joints like these handle end-use parts, or are they only good for early builds?
Both. An early test part and an end-use part follow the same design rules; the difference is how many cycles you test for and which material you pick. HP's fused-powder printing technology is strong enough that many customers ship it as the final part.
What's the easiest way to learn how to design a joint that won't crack?
Start with the itemized specs above, print one test coupon of just the joint, and flex it by hand before committing to a full assembly. It's a faster way to learn how to create something reliable than running simulations alone.
Does a 3D printer need special settings for joint geometry?
Yes. Orientation matters more here than in most parts. Any printer, desktop or industrial, needs a snap-fit joint's arm printed along the X-Y plane rather than up the Z axis, or it inherits the printer's weakest layer bond right where it flexes most.

